

Food-Contact Material & Hygiene Guide
Food-Contact Material & Hygiene Guide
An ultrasonic food cutting machine used in a food plant has to satisfy two different audits at once: the production audit (cut quality, portion weight, pieces per minute) and the hygiene audit (material traceability, surface finish, cleaning access, documentation). Most buyers specify the first in detail and leave the second to the supplier's standard configuration — which is exactly where BRC, IFS and HACCP audits fail. This guide sets out the food-contact material rules that apply to an ultrasonic food cutting machine, explains why the vibrating stack must be titanium alloy rather than stainless steel, and gives you the document package to request before you sign.
1. What "Food Industry Grade" Actually Means
A food grade ultrasonic cutting machine is not a general-purpose cutter with a nicer cover. The difference sits in six places that auditors actually look at. Two machines can cut the same cream cake to identical tolerance and still end up on opposite sides of an audit outcome: one arrives with a folder of material certificates and polished welds, the other fails on a crevice nobody specified.
| Dimension | General-purpose machine | Food industry grade | Why it matters |
| Material traceability | Standard commercial alloy, no certificate | Food-contact material with mill certificate and declaration of compliance | Auditors ask for the certificate, not the description |
| Surface finish | As-machined, Ra 1.6–3.2 μm | Polished to Ra ≤0.8 μm in the product zone | Rougher surfaces hold product residue and biofilm |
| Welds and joints | Functional welds, visible seams | Continuous, ground and polished welds, no crevices | Crevices are the most common non-conformance |
| Cleaning access | Tool strip-down of the cutting head | Quick-release blade holder, tool-free where possible | Strip-down time drives changeover and labour cost |
| Frame and enclosure | Painted steel frame | Washdown-rated frame, smooth and drainable | Washdown is routine in dairy and ready-meal plants |
| Documentation | Manual only | Material list, certificates, cleaning and maintenance plan | This is what turns a machine into an auditable asset |
2. Food-Contact Material Map: Which Part Uses What
Split the ultrasonic food cutting machine into vibrating parts and non-vibrating parts before you write a single material requirement. The vibrating stack — booster, ultrasonic knife body and blade — is governed by acoustics and fatigue, and there is only one material that works. Everything else is governed by cleanability and corrosion, and there you have real choices. Mixing the two groups is how buyers end up asking for a blade material that cannot survive ultrasonic vibration.
| Part | Vibrating? | Material | Governing requirement |
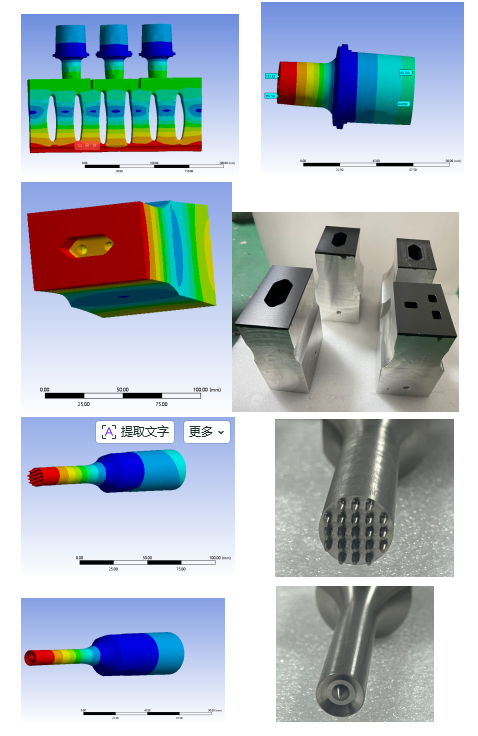
| Booster / sonotrode | Yes | Food-grade titanium alloy Ti-6Al-4V | Acoustic transmission efficiency and fatigue strength at 20–40 kHz |
| Ultrasonic knife body | Yes | Food-grade titanium alloy Ti-6Al-4V | Same acoustic and fatigue requirement as the booster |
| Cutting blade | Yes | Food-grade titanium alloy Ti-6Al-4V; optional food-grade PTFE non-stick coating | Only titanium survives ultrasonic vibration; coating reduces sticking on cheese, nougat and cream |
| Support table / product carrier | No | Food-grade metal or food-grade polymer, Ra ≤0.8 μm | Corrosion against sanitizer and product; cleanability |
| Baffles and guides | No | Food-grade metal or food-grade polymer | No crevices, no product traps |
| Gaskets, belts, press blocks | No | Food-grade silicone, PP, PE or POM with food-contact certificate | Temperature and sanitizer resistance, no plasticizer migration |
| Frame and enclosure | No direct contact | Washdown-rated, corrosion-resistant, smooth and drainable | Daily washdown routine and drain access |
3. Why the Vibrating Stack Must Be Titanium, Not Stainless Steel
The most expensive specification mistake in this product category is asking for a stainless steel blade. Stainless steel is an excellent food-contact material — for a table, a hopper, a frame. It is a poor ultrasonic tool. At 20–40 kHz, stainless steel dissipates vibration energy as heat, work-hardens at the nodal points and loses fatigue strength, so a stainless horn or blade detunes, cracks and loses amplitude. Titanium alloy Ti-6Al-4V is used for the entire vibrating stack because it transmits ultrasonic energy with low loss, holds fatigue strength through millions of cycles, and resists the acid, salt and fat loads of real food products.
| Property | Titanium alloy Ti-6Al-4V | Stainless steel as an ultrasonic tool | What it means for you |
| Acoustic transmission | Low internal loss, amplitude reaches the cutting edge | High internal loss, energy turns into heat | Titanium cuts with less generator load; stainless needs more power for the same cut |
| Fatigue at 20–40 kHz | Holds fatigue strength over long production runs | Work-hardens and cracks, typically at the roots | Blade life and unplanned downtime |
| Weight on the transducer | Light, keeps the stack tuned | Heavy, shifts resonance and detunes the stack | Detuning shows up as unstable cut quality |
| Corrosion vs acid, salt, fat | Stable across dairy, cheese, marinade and high-fat products | Pitting risk under chloride sanitisers | Material choice must match your sanitiser, not just your product |
| Result | Specified for booster, knife body and blade | Not used anywhere in the vibrating stack | If a supplier offers a stainless ultrasonic blade, treat it as a red flag |
4. Surface Finish and Hygienic Design: the Numbers to Write into Your RFQ
Material grade alone will not pass an audit. On an ultrasonic food cutting machine, hygienic design is measurable, and every item below can be written into an RFQ as a number or a yes/no requirement. Write them in before quotation, not after: retrofitting a polished weld or a quick-release holder after delivery is far more expensive than specifying it.
| Requirement | Typical value | Why it matters | How to verify |
| Surface roughness in the product zone | Ra ≤0.8 μm | Below this threshold residue and biofilm are far easier to remove | Ask for a roughness test report on a sample part |
| Welds | Continuous, ground flush and polished, no crevices | Crevices are the single most cited non-conformance | Visual inspection plus weld map drawing |
| Fasteners in the product zone | Avoid exposed threads; use hygienic nuts or covers | Threads harbour product and are hard to clean | Walk the product path during FAT |
| Corners and edges | Rounded, self-draining, no ledges | Flat ledges collect crumb and liquid | Water test after washdown |
| Blade holder strip-down | Quick-release, tool-free where possible, under 2 minutes | Strip-down time drives changeover cost | Time it during acceptance, with your own operator |
| Electrical enclosure | IP54 minimum, IP65 for washdown areas | Water ingress is the top field failure in food plants | Check the rating plate and gland sealing |
| Cleaning access around the cutting zone | Enough clearance for brushes and spray | Inaccessible areas get skipped and fail swab tests | Swab test on the hardest-to-reach point |
5. Non-Metal Contact Parts and Non-Stick Coating
On a food grade ultrasonic cutting machine, polymers and elastomers fail audits more often than metals, because buyers check the metal and assume the rest is fine. Every belt, gasket and press block in the product path needs its own food-contact certificate, and the certificate has to cover your actual cleaning temperature and sanitiser — a silicone rated for 120 °C hot water is not automatically rated for your chlorinated sanitiser.
| Item | Typical material | Certificate to request | Watch out |
| Conveyor belt | Food-grade PU or silicone | Food-contact declaration + temperature range | Belt wear particles are a foreign-body risk |
| Gaskets and seals | Food-grade silicone or EPDM | Food-contact certificate, sanitiser compatibility | Swelling after chemical cleaning causes leaks |
| Press blocks and guides | Food-grade POM or PP | Food-contact certificate | Check wear debris in the product zone |
| Non-stick coating on the blade | Food-grade PTFE | FDA food-contact conformity for the coating | Adhesion matters: peeling coating is foreign-body contamination |
6. Certificates and Documents to Request Before You Sign
Certification for an ultrasonic food cutting machine applies to materials and construction, not to the machine as a single product. What you can legitimately ask for is a material declaration per food-contact part, a conformity statement against the regulation your market uses, and the mill certificate behind it. Ask for these in the RFQ so they arrive with the machine rather than three weeks before your audit.
| Document | What it covers | Who usually asks | What to request |
| FDA 21 CFR conformity | Food-contact substances and materials | US customers, importers | Declaration per part, not per machine |
| EU 1935/2004 (and 10/2011 for plastics) | Framework regulation for food-contact materials | EU customers, customs | Declaration of compliance with migration limits |
| 3-A Sanitary Standards | Hygienic design of food equipment | Dairy and cheese plants | Applies where a 3-A symbol or equivalent design is specified |
| NSF / ANSI 51 | Materials for food equipment | North American food service and retail buyers | Material listing for plastics and coatings |
| Mill / material test report | Actual chemical composition and heat number | Your QA and every serious auditor | Batch-level, traceable to the part |
| HACCP / BRC / IFS support pack | Cleaning plan, material list, maintenance schedule | Plant certification bodies | Ask for the pack your auditor will read, not a brochure |
7. Cleaning, CIP and Changeover: Where the Hours Actually Go
The hygiene argument for an ultrasonic food cutting machine is not only about certificates. A blade that does not smear product across the cut face also carries less residue into the cleaning step, and a quick-release titanium blade holder turns a strip-down into a two-minute job. Over a year, the recovered cleaning and changeover hours often exceed the energy saving that buyers ask about first.
| Step | Conventional blade line | Food-grade ultrasonic line | Time impact |
| Blade residue before cleaning | Smeared cream, cheese and sugar build-up | Thin contact film, most product stays on the portion | Shorter pre-rinse |
| Strip-down | Tools, several fasteners | Quick-release holder, tool-free where possible | Minutes saved per changeover |
| Cleaning method | Manual scrub of blade and guard | Washdown or CIP of the product zone | Lower labour and more repeatable result |
| Verification | Visual check only | Swab or ATP test on defined points | Documented evidence for the auditor |
| Changeover between SKUs | Blade change plus deep clean | Blade change plus parameter recipe | More SKUs per shift |
8. Industries and Products Covered
The same ultrasonic food cutting machine covers most soft, sticky, layered, brittle and frozen products. What changes between industries is not the cutting principle but the hygiene environment: sanitiser type, washdown frequency, product temperature and audit scheme.
| Industry | Typical products | Hygiene pain point | Machine note |
| Bakery | Cream cake, Swiss roll, sponge, bread, croissant | Cream residue on blade, crumb accumulation | 20 kHz, 600–1,000 W, quick-release blade |
| Chocolate and confectionery | Chocolate block, nougat, caramel, fudge | Sugar build-up, temperature-sensitive surface | Non-stick coating, amplitude tuned low |
| Dairy and cheese | Soft cheese, processed cheese, butter, mozzarella | High fat and salt load, daily washdown | Titanium blade, washdown-rated frame |
| Frozen food | Frozen cake, frozen dessert, frozen dough log | Condensation, low-temperature cabling | 20 kHz, 1,000–1,500 W, low-temp cabling |
| Prepared desserts | Mousse, tiramisu, layered dessert, panna cotta | Layer smearing between portions | 30–40 kHz for clean layer separation |
| Energy and cereal bars | Protein bar, granola bar, cereal slice | Sticky binder pulling and tearing | Non-stick coating, higher power |
| Pet food | Semi-moist pet food, treat bar, jerky strip | High fat, odour, frequent cleaning | Easy strip-down, sealed enclosure |
| Plant-based | Plant-based meat block, vegan patty, plant cheese | Acidic marinades, elastic texture | Titanium blade, 20–30 kHz |
| Central kitchen and ready meals | Portioned ready meal, lasagne, rice cake | Multi-SKU changeover, short cleaning window | Parameter recipes, fast changeover |
9. Machine Forms: Handheld, Standalone, Inline and Rotary
Food grade ultrasonic cutting machines come in four hardware forms. Choosing the form first and the power second avoids the most common mismatch: an inline system bought for a volume that a standalone unit would have handled at half the price.
| Form | Power band | Best for | Hygiene note |
| Handheld | 200–500 W | Shops, pastry kitchens, R&D, portion repair | Cable and connector must be wipe-clean |
| Standalone | 600–1,000 W | Medium bakeries and cheese plants, multi-SKU | Quick-release holder, easy access around the table |
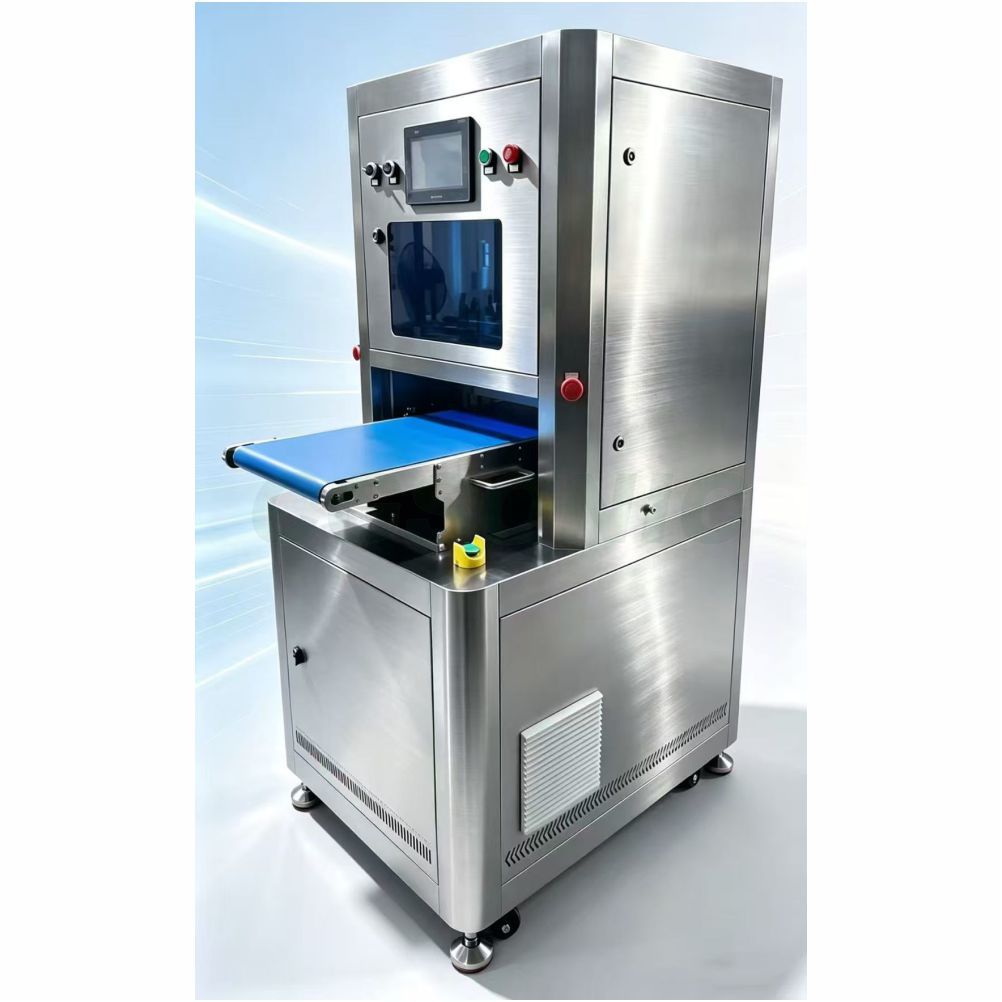
| Inline | 1,000–1,500 W | High-volume continuous lines, fixed SKU | Washdown-rated frame, defined cleaning access |
| Rotary multi-station | 600–1,500 W | Round products, high pieces-per-minute target | More surfaces in the product zone to clean |
10. Technical Parameters
| Parameter | Options | How to choose |
| Frequency | 20 kHz (mainstream) / 30 kHz / 40 kHz | 20 kHz for thicker, tougher and frozen products; 30–40 kHz for thin slices, delicate mousse and high-precision portioning |
| Power | 200–500 W / 600–1,000 W / 1,000–1,500 W | 200–500 W for labs, shops and R&D; 600–1,000 W for cake and bread lines (most common); 1,000–1,500 W for high-viscosity cheese, large blocks and high-speed lines |
| Vibrating stack material | Food-grade titanium alloy Ti-6Al-4V | Specified for booster, knife body and blade; stainless steel is not used in the vibrating stack |
| Blade coating | Bare titanium / food-grade PTFE non-stick | PTFE for sticky products such as cheese, nougat, caramel and cream |
| Generator | Digital generator with amplitude control and parameter storage | Stores a recipe per SKU so changeover is repeatable and auditable |
| Frame and protection | IP54 minimum, IP65 for washdown areas | Match the rating to your actual washdown routine |
| Automation | Servo indexing, conveyor integration, portion weighing, PLC interface | Match line speed and target weight tolerance; this often costs more than the generator |
| Surface finish | Ra ≤0.8 μm in the product zone | Write the number into the RFQ and ask for a test report |
11. A 7-Step Selection Process for Food Plants
- List every product you will cut, with temperature at the cutting station and target portion weight tolerance.
2. Classify each product: soft, sticky, layered, brittle, frozen or elastic. This decides frequency and blade geometry.
3.Define the hygiene environment: sanitiser type, washdown frequency, IP rating and audit scheme (BRC, IFS, HACCP, 3-A).
4. Fix the material requirements in the RFQ: titanium for the vibrating stack, Ra ≤0.8 μm in the product zone, food-contact certificates for every polymer.
5.Choose the machine form from volume and SKU count: handheld, standalone, inline or rotary multi-station.
6. Request the document package: material declarations, conformity statements, mill certificates, cleaning plan and maintenance schedule.
7. Run a sample cutting test on your own product and keep the report — cut-face photos, portion weights, cycle times — as the acceptance baseline.
12. Five Procurement Mistakes
| Mistake | Why it happens | Consequence | Fix |
| Asking for a stainless steel cutting blade | Stainless is the default metal in food plants | Detuning, cracking, lost amplitude, short blade life | Specify titanium alloy Ti-6Al-4V for the whole vibrating stack |
| Only specifying metal, ignoring polymers | Belts and gaskets look like minor parts | Audit finding on an uncertified gasket | Request a food-contact certificate for every non-metal contact part |
| Accepting the supplier's standard frame | Frame is treated as packaging, not as equipment | Rust and water ingress within one washdown season | Specify washdown rating and IP class in the RFQ |
| Skipping the sample cutting test | Schedule pressure and a good-looking datasheet | Cut quality or throughput discovered too late | Make the sample report a contractual acceptance item |
| Buying inline capacity for standalone volume | Buying headroom for future growth | Over-specification, longer payback, harder cleaning | Size the machine to today's volume plus one defined growth step |
13. The RFQ Document Package: What to Ask Your Supplier
Send this list with your ultrasonic food cutting machine enquiry. Suppliers who answer it in full are usually the ones whose machines pass audit without a second visit.
- Material declaration for every food-contact part, including the booster, knife body, blade, table, gaskets and belts.
- Mill certificate with heat number for the titanium alloy used in the vibrating stack.
- Conformity statement against FDA 21 CFR, EU 1935/2004 (and 10/2011 for plastics), 3-A or NSF/ANSI 51 as your market requires.
- Surface roughness test report for the product zone, target Ra ≤0.8 μm.
- Weld map and hygienic design statement: continuous welds, no crevices, no exposed threads in the product path.
- Strip-down procedure with measured time, plus the cleaning and sanitising plan.
- IP rating of the electrical enclosure and the recommendation for washdown areas.
- Sample cutting report: cut-face photos, portion weights, cycle times, recommended frequency, power, blade geometry and coating.
14. Cost, Lead Time and Payback
Buyers usually compare ultrasonic food cutting machines on generator price. In practice the cost drivers are the automation, the hygienic construction and the documentation package — and the payback comes mostly from recovered product and recovered cleaning hours.
| Cost or benefit item | What drives it | Note for the buyer |
| Generator and stack | Power band, frequency, titanium grade | The smallest part of a full project budget |
| Blades and holders | Geometry, coating, number of SKUs | Plan as scheduled consumables, keep one spare set |
| Automation | Servo indexing, conveyor, weighing, PLC | Often costs more than the generator |
| Hygienic construction | Polishing, weld finishing, washdown frame, IP class | Cheap to specify now, expensive to retrofit |
| Documentation | Certificates, reports, cleaning plan | Free at quotation, slow and painful after delivery |
| Payback | Waste reduction, portion accuracy, cleaning hours | Measure on your own SKU, not on a supplier average |
15. Eight-Question Self-Check Before You Enquire
|
# |
Question |
If yes |
|
1 |
Do you know the material of every food-contact part you are about to buy? |
If not, stop and ask for the material map |
|
2 |
Is the vibrating stack specified as titanium alloy Ti-6Al-4V? |
Correct; if a stainless blade was offered, query it |
|
3 |
Is Ra ≤0.8 μm written into the RFQ for the product zone? |
Ask for a roughness test report |
|
4 |
Do all belts, gaskets and press blocks have food-contact certificates? |
Request certificates per part |
|
5 |
Is the frame washdown-rated for your cleaning routine? |
Confirm IP rating and drain access |
|
6 |
Can your operator strip the blade in under two minutes? |
Time it during acceptance |
|
7 |
Do you have the document package your auditor will read? |
Add it to the RFQ before signing |
|
8 |
Have you run a sample cutting test on your own product? |
Keep the report as the acceptance baseline |
16. Final Summary
A food industry ultrasonic food cutting machine is specified in two layers: acoustics for the vibrating stack, hygiene for everything else. Get the first layer right by specifying titanium alloy Ti-6Al-4V for the booster, knife body and blade; get the second right by writing surface finish, weld quality, cleaning access and certificates into the RFQ instead of assuming them. The machine that cuts well and the machine that passes audit are the same machine — but only if both layers are specified.
Send us your product list, sanitiser and cleaning routine, target portion weight and pieces per minute. We will return a material map, a recommended frequency and power band, the document package, and a sample cutting report before any order is placed.
17. FAQ
Q: Is the blade of an ultrasonic food cutting machine made of stainless steel or titanium?
A: Titanium. The booster, the ultrasonic knife body and the blade are all food-grade titanium alloy Ti-6Al-4V, because stainless steel does not work as an ultrasonic tool: at 20–40 kHz it dissipates energy as heat, work-hardens and loses fatigue strength, so a stainless horn or blade detunes, cracks and loses amplitude. Stainless steel remains an excellent material for non-vibrating parts such as tables, frames and enclosures, but it is not used anywhere in the vibrating stack.
Q: Does the machine come with FDA, 3-A or NSF certification?
A: Certification applies to materials and hygienic construction, not to the machine as one product. What you should receive is a material declaration for each food-contact part, a conformity statement against the regulation your market uses (FDA 21 CFR, EU 1935/2004, 3-A Sanitary Standards or NSF/ANSI 51), and the mill certificate behind the titanium and polymer parts. This documentation is what supports BRC, IFS and HACCP audits.
Q: What surface finish should I specify for food contact?
A: Ra ≤0.8 μm in the product zone is the common requirement, together with continuous welds ground flush and polished, no crevices and no exposed threads above the product path. Ask for a roughness test report on a sample part rather than a verbal confirmation, and add rounded, self-draining surfaces so nothing pools after washdown.
Q: Can an ultrasonic food cutting machine be CIP or washdown cleaned?
A: The product zone can be specified for washdown and, on inline machines, for CIP routines. The ultrasonic stack itself — transducer, booster and blade — is a precision assembly: it is removed for cleaning and must not be immersed or pressure-washed while connected. Define your sanitiser, concentration and temperature in the RFQ so the seals, coatings and polymer parts are selected against the chemicals you actually use.
Q: Which frequency and power do I need for my products?
A: 20 kHz is the mainstream choice for bakery, cheese, confectionery and frozen products. 30 kHz and 40 kHz are specified for thin slices, delicate mousse and tight portion tolerances. Power follows the product and the throughput: 200–500 W for labs, shops and R&D, 600–1,000 W for cake and bread lines, 1,000–1,500 W for high-viscosity cheese, large blocks and high-speed lines. Confirm the final choice with a sample cutting test.
Q: Can one ultrasonic food cutting machine handle several products?
A: Usually yes. By changing blade geometry, frequency and stored parameter recipes, one machine can run cream cake, sticky nougat, soft cheese and frozen dessert on the same frame. The limits are mechanical: maximum board size, product height clearance and changeover time. If you run many SKUs, ask for stored recipes and a quick-release holder so changeover stays repeatable.
Q: Can it be integrated into an existing line?
A: Yes. Most retrofit projects keep the existing conveyor and packaging equipment and add an ultrasonic cutting station: generator, transducer, booster and blade, plus servo indexing where portion control is required. The three checks that matter are line speed matching, product height clearance, and cleaning access around the cutting zone.
Q: How do I start an evaluation?
A: Send your product list with photos or cross-sections, product temperature at the cutting station, target portion weight and tolerance, pieces per minute, your sanitiser and cleaning routine, and whether you need handheld, standalone, inline or rotary. A serious supplier returns a material map, a recommended configuration and a sample cutting report with cut-face photos and measured portion weights.